Real-Time Machine Monitoring
Connect machines and industrial equipment with IoT sensors to monitor temperature, vibration, pressure, speed, energy consumption, operating conditions, and other critical parameters.
Industrial IoT Solutions
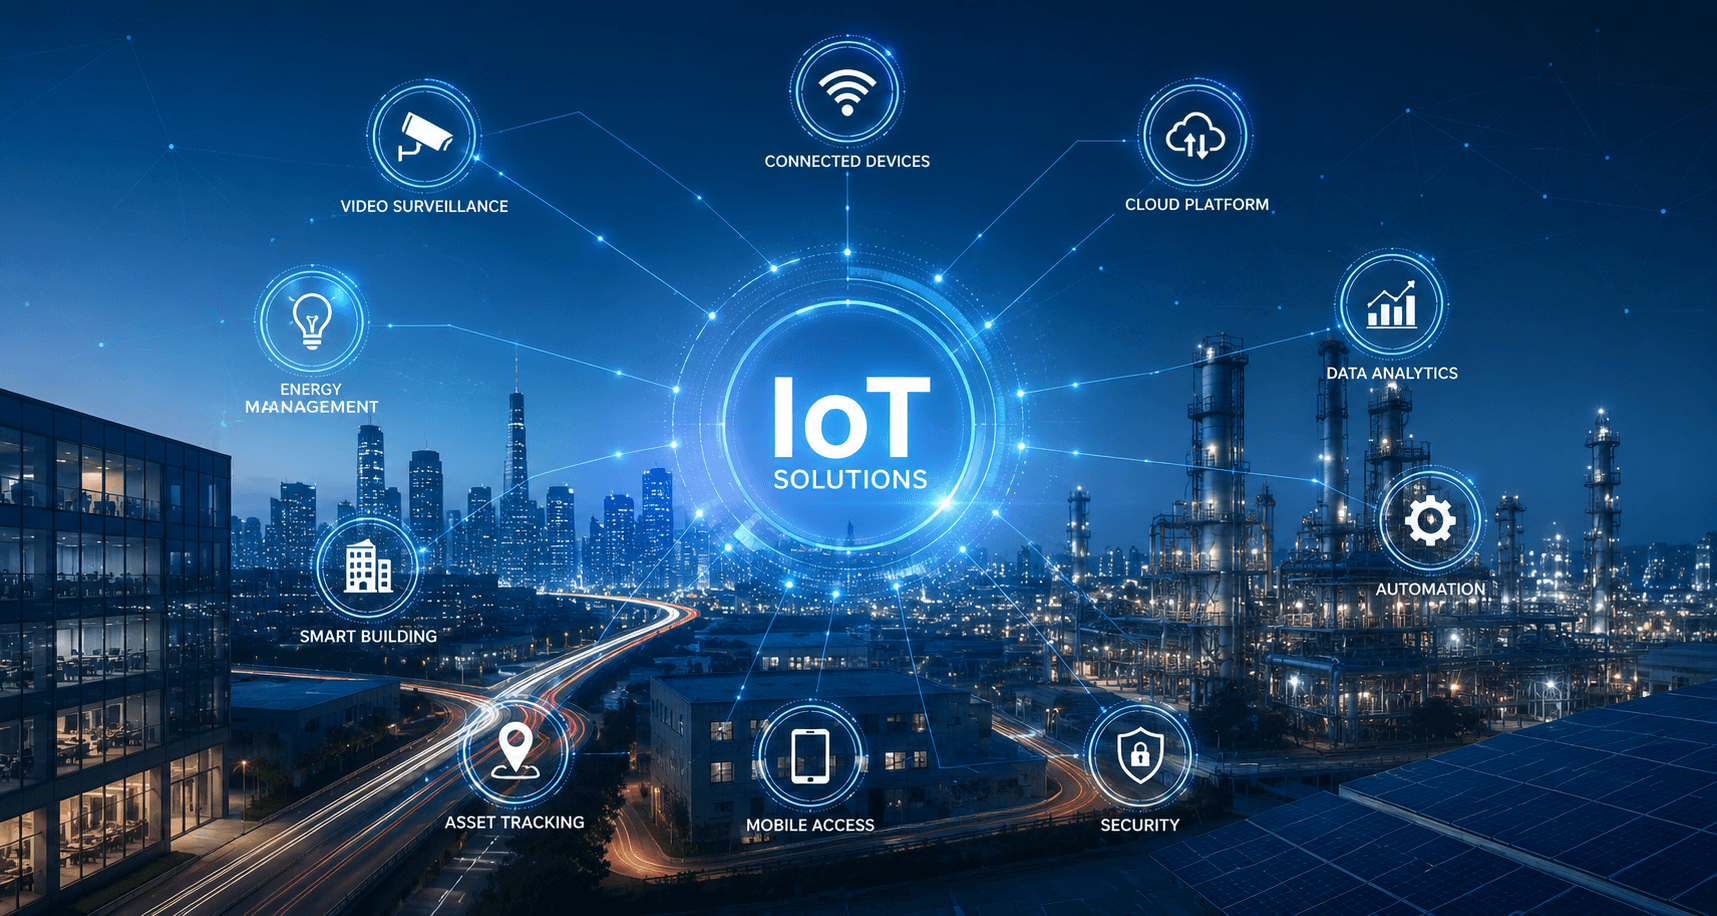
The modern manufacturing industry is moving toward connected machines, intelligent automation, real-time monitoring, and data-driven decision-making. Industrial IoT solutions enable businesses to connect machines, equipment, assets, inventory, and enterprise systems to create a unified digital industrial ecosystem.
What Are Industrial IoT Solutions?
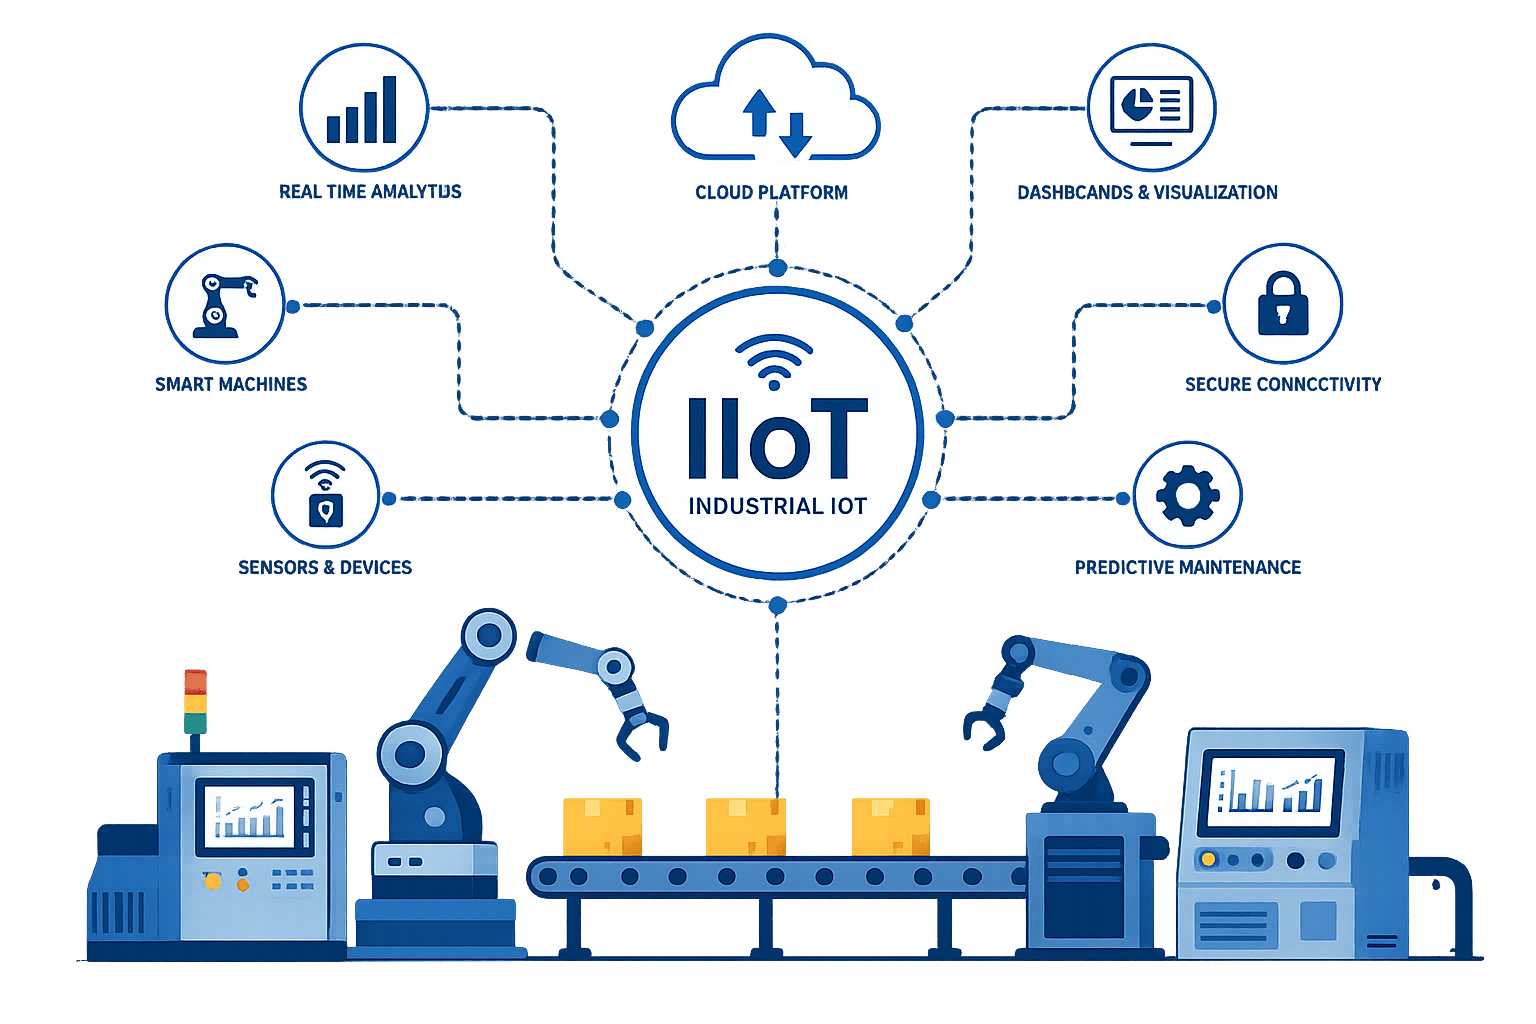
Industrial IoT, or IIoT, connects industrial equipment and physical assets with sensors, software platforms, communication networks, and data analytics systems.
Instead of relying on isolated machines and manual processes, organizations can create a connected environment where operational data is continuously collected, processed, analyzed, and shared across relevant teams. This enables businesses to move from reactive operations toward proactive and predictive decision-making.
Machine performance
Production output
Equipment health
Inventory levels
Material movement
Asset utilization
Energy consumption
Warehouse operations
Maintenance requirements
Production efficiency
How Industrial IoT Is Transforming Manufacturing
Industrial IoT is becoming a critical technology for organizations looking to improve productivity, operational visibility, and resource utilization.
Connect machines and industrial equipment with IoT sensors to monitor temperature, vibration, pressure, speed, energy consumption, operating conditions, and other critical parameters.
Analyze machine data to identify unusual behavior and potential equipment failures before they cause costly production downtime.
Track production output, machine utilization, cycle times, downtime, operational efficiency, and other manufacturing KPIs through centralized dashboards.
Connect inventory, warehouse, equipment, and production systems to improve visibility into raw materials, components, spare parts, work-in-progress, and finished goods.
Monitor the location, movement, utilization, and status of critical assets across manufacturing facilities and warehouses.
Track energy consumption across machines, production lines, and facilities to identify inefficiencies and optimize industrial energy usage.
Use IoT data and business rules to automate alerts, maintenance workflows, inventory actions, approvals, and operational processes.
Industrial IoT Solution Capabilities
Our industrial IoT solutions can be customized to address different manufacturing, industrial, warehouse, and asset management requirements.
Connect machines, sensors, PLCs, gateways, meters, RFID readers, GPS trackers, cameras, and other industrial devices.
Collect and visualize real-time equipment data to monitor machine health and performance.
Use sensor data, analytics, and AI to identify potential equipment problems and optimize maintenance planning.
Monitor stock levels, material movement, warehouse conditions, and inventory locations.
Track valuable equipment, tools, containers, materials, vehicles, and other industrial assets.
Monitor production performance and identify operational bottlenecks using real-time data.
Configure intelligent alerts based on equipment conditions, inventory thresholds, environmental parameters, or business rules.
Provide managers, engineers, operators, and business teams with role-specific dashboards and operational KPIs.
Integrate IoT platforms with ERP, CRM, inventory management software, warehouse management systems, and maintenance platforms.
Apply AI and machine learning to industrial data for anomaly detection, forecasting, predictive maintenance, and operational optimization.
Industrial IoT Inventory Management
Inventory visibility is a major challenge for manufacturing and industrial organizations. Manual inventory processes can make it difficult to know exactly what materials are available, where they are located, how much is being consumed, and when replenishment is required.
An IoT-enabled inventory management system connects physical inventory with digital systems to provide real-time visibility across warehouses, production facilities, storage locations, and supply chains.
Our solutions can help organizations implement intelligent inventory tracking management using technologies such as RFID, QR codes, BLE, GPS, sensors, and connected devices.
Real-time inventory visibility
Automated stock updates
Warehouse monitoring
Low-stock alerts
Material tracking
Spare parts management
Inventory analytics
Inventory Management Software With IoT
Traditional inventory management software primarily depends on manual data entry, barcode scanning, or periodic stock updates. Integrating IoT technologies can take inventory management to the next level.
An IoT-enabled inventory platform can continuously capture data from connected devices and synchronize it with your central software system. This reduces dependence on manual inventory processes while improving the accuracy and timeliness of operational information.
Real-time stock visibility
Automated inventory tracking
Location-based asset visibility
Material movement tracking
Warehouse monitoring
Stock-level alerts
Automated replenishment triggers
Consumption analytics
Inventory forecasting
Production material visibility
Spare parts monitoring
Audit trails
Industrial IoT Use Cases
Industrial IoT can be applied across multiple areas of manufacturing and industrial operations.
Connect production machines and equipment to monitor output, performance, downtime, and operational efficiency.
Monitor machine health continuously and identify early warning signs of equipment failure.
Use IoT-enabled tracking to improve inventory visibility, material movement, warehouse utilization, and storage management.
Track materials, products, containers, and assets throughout the industrial supply chain.
Monitor environmental and operational conditions that can affect product quality and manufacturing processes.
Measure and analyze energy consumption across facilities and production equipment.
Monitor temperature, humidity, location, and other environmental conditions for temperature-sensitive materials and products.
Use connected devices and sensors to monitor industrial environments and support safety-related processes.
Benefits of Industrial IoT
Implementing Industrial IoT can deliver significant improvements across production, maintenance, inventory, and operational management.
Real-time monitoring and predictive maintenance help identify potential problems before they become major failures.
Monitor machine utilization, production performance, and operational bottlenecks to improve overall efficiency.
Improve inventory accuracy and reduce excess stock, shortages, misplaced materials, and unnecessary manual processes.
Use real-time data to identify resource inefficiencies, unnecessary downtime, energy waste, and maintenance costs.
Give decision-makers access to real-time operational information through dashboards, reports, and analytics.
Understand where assets are located, how they are being used, and when they require maintenance or replacement.
Create a centralized digital view of machines, assets, inventory, production, and other industrial operations.
Technologies Behind Our Industrial IoT Solutions
Our IIoT architecture can integrate a wide range of technologies depending on the operational environment and business requirements.
Capture machine, environmental, equipment, inventory, and operational data in real time.
Identify and track inventory, assets, tools, containers, and materials throughout industrial facilities.
Collect data from multiple machines and devices and securely transmit it to cloud or enterprise platforms.
Process, store, visualize, and analyze large volumes of industrial IoT data through scalable cloud infrastructure.
Analyze historical and real-time industrial data to identify patterns, anomalies, and predictive insights.
Transform raw IoT telemetry into dashboards, KPIs, reports, trends, and actionable business intelligence.
Our Industrial IoT Development Services
Implementing IIoT successfully requires more than connecting devices. It requires a clear technology strategy, scalable architecture, secure integrations, and an understanding of industrial workflows. Our internet of things consulting services help organizations identify high-value IoT opportunities and create a practical roadmap for implementation.
Industrial IoT Consulting
IIoT Strategy & Roadmap
IoT Architecture Design
IoT Device Integration
Machine Connectivity
Industrial Sensor Integration
IoT Platform Development
Inventory Monitoring Solutions
Asset Tracking Solutions
Predictive Maintenance Solutions
IoT Dashboard Development
Industrial Mobile Applications
IoT Data Analytics
AI & Machine Learning Integration
Enterprise System Integration
IoT Security
IoT Support & Maintenance
Whether you are modernizing an existing manufacturing environment or building a new connected industrial platform, we can help you design and implement an IIoT ecosystem aligned with your business objectives.
Why Choose Us for Industrial IoT?
Industrial IoT projects require expertise across hardware connectivity, software engineering, cloud infrastructure, data analytics, enterprise integration, and industrial operations.
From consulting and architecture to development, deployment, integration, and support, we cover the complete IoT lifecycle.
We design solutions around your machines, workflows, inventory processes, assets, and operational requirements.
Our platforms can scale from individual facilities to multi-site industrial operations with thousands of connected devices.
Monitor equipment, production, inventory, and assets through centralized dashboards and applications.
Connect your IoT ecosystem with existing ERP, inventory, maintenance, warehouse, and business applications.
Security, device authentication, access control, data protection, monitoring, and reliable communication are considered throughout the solution architecture.
The Future of Manufacturing Is Connected
The future of the manufacturing industry will be driven by connected machines, intelligent automation, real-time data, and predictive decision-making.
Industrial IoT provides the foundation for this transformation by connecting physical operations with digital intelligence. When machines, inventory, assets, and enterprise systems work together, organizations gain the visibility needed to improve productivity, reduce costs, and respond faster to changing operational conditions.
Whether your objective is predictive maintenance, smart inventory management, production monitoring, asset tracking, or complete factory digitization, industrial IoT solutions can help you create a more connected and intelligent operation.
Build Your Industrial IoT Solution
Looking to modernize your manufacturing operations, improve inventory visibility, or connect your industrial assets? Our IoT specialists can help you identify the right use cases, technologies, architecture, and implementation strategy for your organization.